Digital Printing on Fabric: Process, Benefits, and Applications
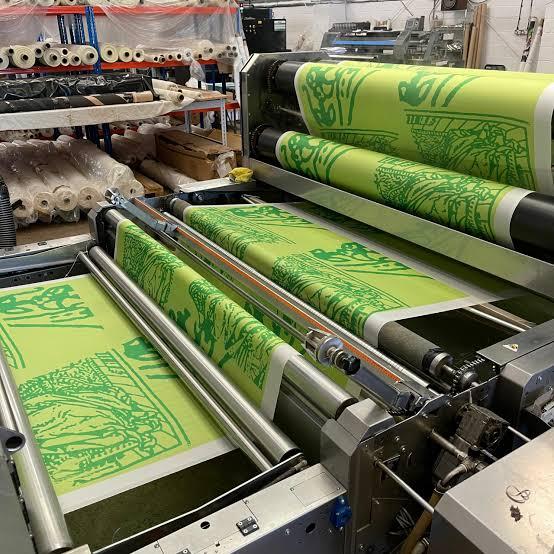
Digital printing on fabric is a modern textile printing method that transfers digital artwork directly onto fabric using specialized inkjet printers. Unlike traditional printing methods that often require screens, plates, or engraved rollers, digital systems can reproduce detailed designs directly from a computer file. This makes the process useful for fashion, home textiles, custom products, interior decoration, and small-batch production.
The growth of Digital printing on fabric has changed how textile designs are developed and produced. Designers can create complex patterns, photographs, gradients, and fine details without preparing a separate screen for every color. The technology also supports shorter production runs, customization, and faster design changes. However, achieving good results depends on choosing the right ink, fabric, pretreatment, printer settings, and finishing process.
What Is Digital Fabric Printing?
Digital fabric printing is an inkjet-based process in which a printer deposits tiny droplets of textile ink onto a fabric surface according to a digital image file. The printer controls the placement and quantity of ink to reproduce colors, shapes, and details.
The fabric is usually prepared before printing because untreated fibers may absorb ink unevenly. After printing, some fabric types require additional fixation through heat, steaming, or another appropriate curing method. Washing or finishing may then be carried out to remove unfixed substances and improve the fabric's final properties.
How the Printing Process Works
The process generally involves several stages:
- Design preparation: Artwork is created or adjusted using graphic design software. Color profiles and image resolution are checked before production.
- Fabric selection: The material is selected according to its fiber composition and intended use.
- Pretreatment: Depending on the ink technology, the fabric may receive a chemical treatment that helps control ink absorption and improve color development.
- Printing: The digital printer applies textile ink directly to the fabric.
- Fixation: The printed fabric undergoes the appropriate heat, steam, or curing process so the color bonds properly with the fibers.
- Washing and finishing: Some processes require washing to remove excess chemicals or unfixed dye before the fabric is dried and finished.
The exact procedure varies according to whether pigment, reactive, acid, or sublimation inks are being used.
Types of Digital Fabric Printing
Different textile fibers require different printing technologies. There is no single ink system that works equally well for every fabric.
Reactive Printing
Reactive inks are commonly used with cellulose-based fabrics such as cotton, linen, rayon, and some other regenerated fibers. The dye chemically reacts with the fiber during fixation, producing strong color penetration and good wash durability.
Reactive printing is particularly suitable for clothing, bed linen, scarves, and other products where softness and frequent washing are important.
Pigment Printing
Pigment inks can be used on a broad range of textiles. They are applied to the fabric surface and normally require a binder and heat curing to secure the pigment.
One advantage of pigment printing is that it can reduce the number of wet-processing stages compared with some dye-based methods. It is useful for cotton and blended fabrics, particularly when production flexibility is important.
Acid Printing
Acid inks are primarily associated with protein fibers such as silk and wool, as well as certain polyamide fabrics. They can produce bright colors and detailed designs when the fabric and process are properly prepared.
This technology is often used for fashion fabrics, scarves, swimwear, and other products where these fibers are appropriate.
Dye-Sublimation Printing
Sublimation printing is widely used for polyester fabrics. The design is first printed onto transfer paper or, in some systems, directly onto polyester fabric. Heat causes the dye to convert into a gas and penetrate the polyester fibers.
It is commonly used for sportswear, flags, banners, soft signage, and promotional textiles. The process is particularly effective for polyester because the dye becomes integrated into the fiber rather than simply sitting on its surface.
Key Benefits of Digital Printing on Fabric
Detailed and Complex Designs
Digital printers can reproduce fine lines, photographic images, gradients, and numerous colors without creating individual screens for each color. This gives designers greater freedom when developing intricate patterns.
Suitable for Small Production Runs
Traditional textile printing can involve significant setup work, making very small orders less economical. Digital printing reduces much of this preparation, which makes customized products and short production runs more practical.
Faster Design Changes
A new digital file can be prepared and sent to the printer without manufacturing a new screen or engraving a new roller. This helps businesses produce samples and modify designs more efficiently.
Personalization
Digital systems are well suited to variable designs. For example, a business can produce personalized scarves, custom clothing, printed cushions, or limited-edition textile collections without changing the fundamental printing setup.
Reduced Setup and Material Waste
Digital printing can avoid some of the screens, plates, and setup materials associated with conventional printing. It can also reduce waste when producing samples or small quantities because manufacturers do not need to prepare large production runs simply to justify setup costs.
Practical Factors That Affect Print Quality
Good digital fabric printing requires more than a high-resolution printer.
Fabric Preparation
Fabric construction, fiber type, weight, and surface condition all influence how ink behaves. A fabric that absorbs ink too quickly may produce blurred edges, while an unsuitable surface can cause poor adhesion or uneven color.
Color Management
The colors displayed on a computer monitor do not automatically match the printed result. Proper color profiling, calibrated equipment, suitable ink, and controlled production conditions help reduce color differences.
Artwork Resolution
Low-resolution images may appear pixelated or soft when enlarged. For detailed textile designs, artwork should be prepared at an appropriate resolution for the intended print size.
Ink and Fabric Compatibility
The ink must be compatible with the textile fiber. Using an unsuitable combination can lead to weak color, poor wash resistance, cracking, bleeding, or inadequate adhesion.
Common Challenges and Considerations
Digital printing offers flexibility, but it also has limitations. Equipment and specialized inks can require significant investment. Production speed can vary by printer, fabric, image coverage, and required quality level. Some processes also require pretreatment, steaming, washing, or curing equipment.
Color consistency can become challenging during long production runs. Environmental conditions, fabric batches, ink characteristics, and machine calibration can all influence the final appearance. Businesses therefore need quality-control procedures to maintain consistent results.
Cost should also be evaluated carefully. Digital printing may be attractive for samples and smaller orders, while conventional printing can remain competitive for very large quantities of a repeating design. The appropriate method depends on order size, fabric type, design complexity, turnaround requirements, and finishing needs.
Applications of Digital Fabric Printing
Digital printing is used across several textile markets.
- Fashion: Dresses, shirts, scarves, skirts, and designer fabrics.
- Home textiles: Curtains, cushions, bedding, table linens, and upholstery fabrics.
- Sportswear: Custom jerseys, athletic clothing, and team uniforms, particularly with polyester sublimation.
- Interior decoration: Wall coverings, decorative fabrics, and customized furnishings.
- Promotional products: Flags, banners, fabric displays, and branded textile items.
- Sampling: Designers can test patterns and color combinations before committing to larger production quantities.
Frequently Asked Questions
1. Is digital printing suitable for cotton?
Yes. Cotton can be digitally printed using technologies such as reactive or pigment printing. The correct choice depends on the required softness, color strength, durability, production process, and equipment.
2. Does digital fabric printing last after washing?
It can. Durability depends on the ink technology, fabric, pretreatment, fixation, and washing conditions. Properly processed reactive prints, for example, can provide strong wash durability on suitable cellulose fabrics.
3. Can photographs be printed on fabric?
Yes. Digital printers can reproduce photographic images, gradients, shadows, and fine details. The quality of the original artwork and the printer's capabilities affect the final result.
4. Is digital printing better for small orders?
Digital printing is often well suited to small and customized orders because it requires less setup than many conventional printing methods. However, cost advantages depend on the specific fabric, printer, ink, and production requirements.
5. Which fabrics can be digitally printed?
Different technologies support different fibers. Cotton and other cellulose fabrics can be printed with reactive or pigment systems, polyester is commonly printed using sublimation, and silk, wool, and some polyamides can be printed with acid inks.
Conclusion
Digital printing on fabric provides textile manufacturers and designers with a flexible way to produce detailed, customized, and short-run designs. Its ability to print directly from digital artwork reduces certain setup requirements and makes rapid sampling and personalization more practical.
The best results depend on matching the printing technology with the fabric and intended application. Proper pretreatment, color management, fixation, finishing, and quality control are equally important. While digital printing is not automatically the most economical choice for every production volume, its combination of design flexibility, customization, and efficient sampling makes it an important technology in modern textile production.

 English
 Arabic
 French
 Spanish
 Portuguese
 Deutsch
 Turkish
 Dutch
 Italiano
 Russian
 Romaian
 Greek