Cost-Effective Metal Detection Systems for Business Operations
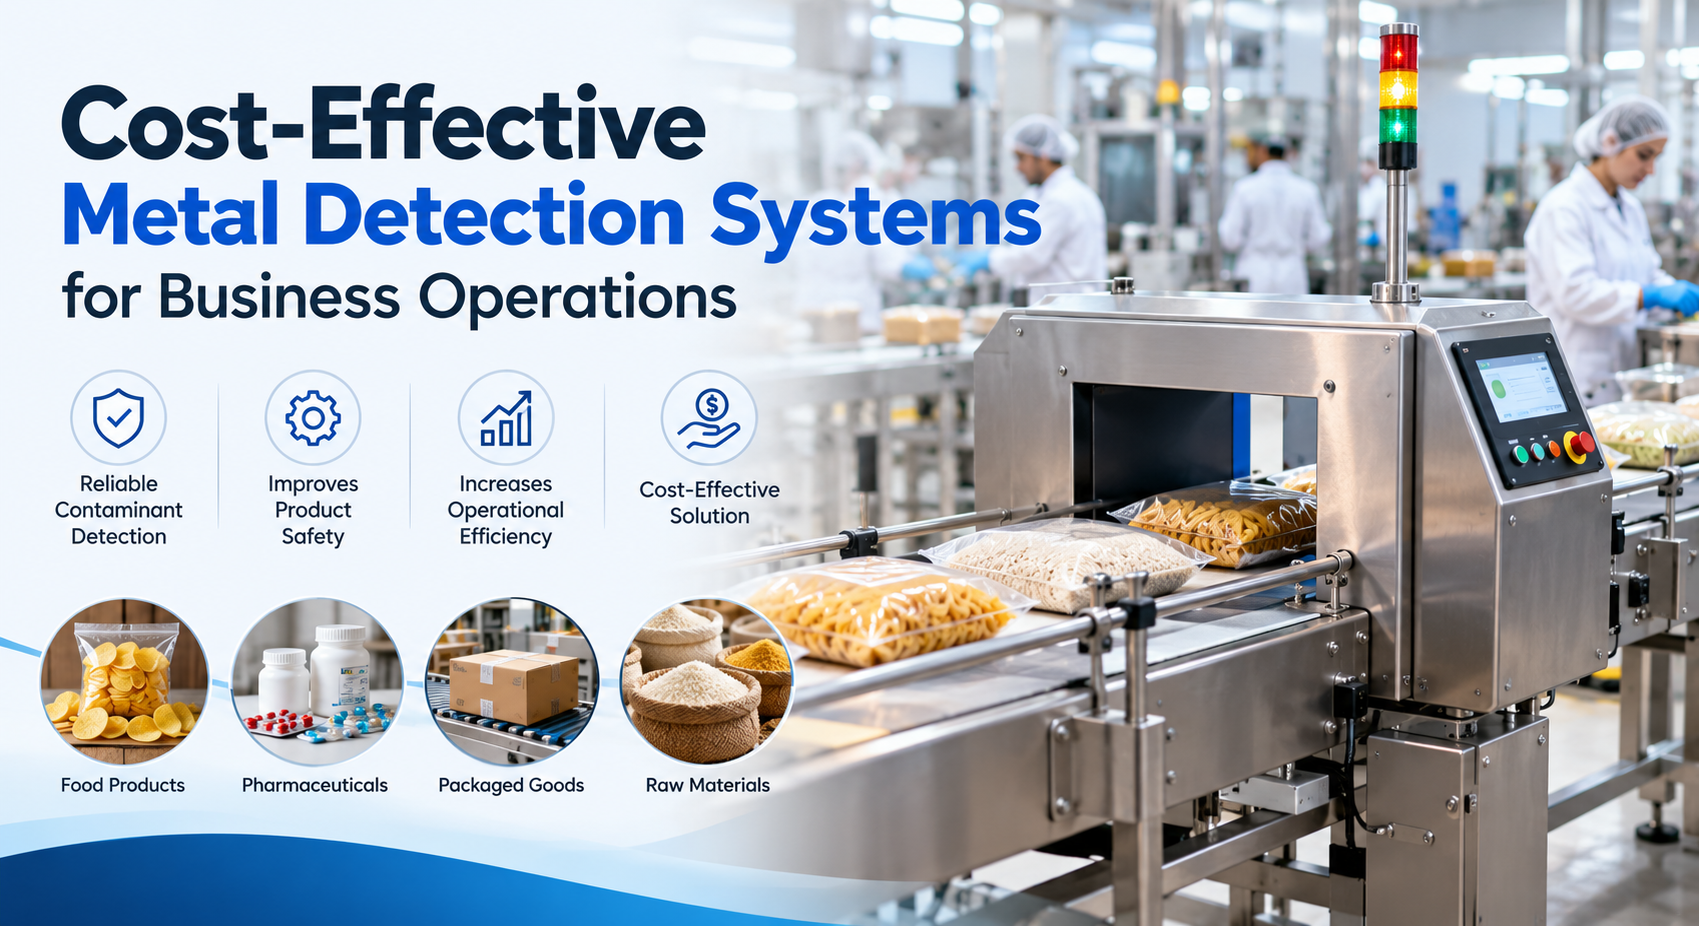
Metal detection systems play an important role in maintaining product quality, workplace safety, and operational efficiency across various industries. From food processing and pharmaceutical manufacturing to packaging and industrial production, businesses rely on metal detection technology to identify unwanted metallic contaminants before products reach customers. Investing in cost-effective metal detection systems helps organisations reduce product losses, maintain quality standards, and protect their reputation without exceeding their operational budgets.
NOTE :- Businesses had relied on Metal detector suppliers in UAE to improve operational safety and product inspection. Al Jarah Industries had helped industrial operations identify suitable metal detection equipment for their specific applications. Connect with Al Jarah Industries to discuss your requirements and discover reliable solutions for industrial inspection.
Understanding Metal Detection Systems
Metal detection systems are specialised devices designed to identify metallic contaminants in products, materials, or production environments. These systems use electromagnetic fields to detect metal particles, including ferrous metals, non-ferrous metals, and stainless steel, depending on the equipment's design and sensitivity.
Modern metal detectors are available in different configurations to suit specific industrial applications. Conveyor-based systems inspect products moving along production lines, while pipeline detectors examine liquid, paste, and slurry products. Gravity-fed detectors are commonly used for powders and granular materials. Selecting the appropriate system depends on the product characteristics, production speed, contamination risks, and required detection accuracy.
Why Cost-Effective Metal Detection Matters
Businesses must balance product safety, operational performance, and equipment investment. A cost-effective metal detection system offers reliable performance while helping control initial purchasing expenses and ongoing maintenance costs.
Reducing Product Waste and Financial Losses
Metal contamination can result in rejected batches, product recalls, production interruptions, and financial penalties. Early detection helps identify contaminated products before they move further through the manufacturing process. This reduces unnecessary waste and limits the cost of reprocessing or disposing of affected materials.
Improving Product Quality and Customer Confidence
Consistent inspection supports quality control procedures and helps businesses deliver products that meet customer expectations. Reliable detection processes can also strengthen customer confidence, protect brand reputation, and support compliance with applicable industry requirements.
Supporting Operational Efficiency
Automated metal detection systems can inspect products continuously without significantly slowing production when correctly selected and integrated. This allows businesses to maintain production targets while reducing dependence on manual inspection methods.
Key Features to Consider When Choosing a System
Selecting the right equipment involves evaluating several technical and operational factors rather than focusing exclusively on the purchase price.
Detection Sensitivity and Accuracy
Detection sensitivity determines the size and type of metal contaminants a system can identify under specific operating conditions. Businesses should choose equipment that meets their product safety requirements without paying for unnecessary capabilities. Product characteristics, including moisture, temperature, packaging material, and conductivity, may influence detection performance.
Production Capacity and Integration
The selected detector should match the speed, volume, and configuration of the existing production line. Conveyor systems, pipeline units, and free-fall detectors should integrate smoothly with current machinery. Proper integration reduces installation difficulties and minimises production downtime.
Maintenance and Operating Costs
A cost-effective system should be easy to clean, inspect, calibrate, and maintain. Businesses should consider spare parts availability, service support, energy consumption, and the expected lifespan of the equipment. Evaluating these expenses helps determine the total cost of ownership rather than relying solely on the initial purchase price.
Applications Across Different Industries
Metal detection technology supports quality control in several industrial sectors. In food processing, it helps identify metallic contaminants in packaged foods, meat, dairy products, snacks, and bulk ingredients. Pharmaceutical manufacturers use appropriate inspection systems to help protect product integrity and support established quality procedures.
In packaging and manufacturing facilities, metal detectors inspect materials and finished products for unwanted metallic particles. Chemical processing, plastics production, and recycling operations may also use specialised systems to identify metal contamination or separate metallic materials, depending on their operational requirements.
Each application requires equipment designed for its specific environment. Factors such as product consistency, conveyor speed, operating temperature, cleaning procedures, and contamination risks should guide equipment selection.
Strategies for Maximising Cost Efficiency
Businesses can improve the financial value of metal detection systems through careful planning and regular performance evaluation. Conducting a contamination risk assessment before purchasing equipment helps identify critical inspection points and prevents unnecessary investment in unsuitable machinery.
Preventive maintenance is another important strategy. Routine testing, calibration, cleaning, and component inspections help maintain detection reliability and reduce the likelihood of unexpected equipment failures. Staff training also ensures that operators understand correct procedures for testing, handling rejected products, and responding to alarms.
Additionally, businesses should compare equipment suppliers based on technical specifications, warranty coverage, after-sales service, installation support, and replacement part availability. A supplier offering dependable technical assistance can help reduce downtime and long-term operating expenses.
Evaluating Return on Investment
The financial benefits of metal detection systems extend beyond contamination prevention. Businesses should evaluate potential savings from reduced product recalls, lower material waste, fewer rejected batches, improved production continuity, and reduced quality-related expenses.
A system with a higher initial price may provide better long-term value if it offers greater reliability, lower maintenance requirements, and improved detection performance. Conversely, a smaller operation may benefit from a simpler system that meets its essential inspection requirements without unnecessary features.
Calculating the expected return on investment helps businesses make informed purchasing decisions and select equipment that supports their financial and operational objectives.
Conclusion
Cost-effective metal detection systems are valuable investments for businesses seeking to improve product quality, strengthen contamination control, and maintain efficient production operations. By considering detection accuracy, production requirements, maintenance expenses, and long-term performance, organisations can choose solutions that deliver dependable results within their budgets. A well-selected and properly maintained metal detection system supports safer products, reduces avoidable losses, and contributes to sustainable business growth.
For More Insightful Articles Related To This Topic, Feel Free To Visit: https://kontentz.xzero.co.uk/

 English
 Arabic
 French
 Spanish
 Deutsch
 Turkish
 Dutch
 Italiano
 Russian
 Romaian
 Portuguese (Brazil)
 Greek